Flat-Bed vs. Slant-Bed CNC Lathe: What’s the Difference and Which One Do You Need?
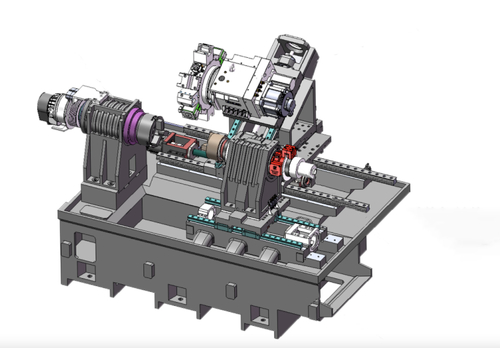
Flat-Bed vs. Slant-Bed CNC Lathe: What’s the Difference and Which One Do You Need?
Comparing machine design, machining capabilities, accuracy, and cost
Both flat-bed and slant-bed CNC lathes can turn outside diameters, face parts, bore holes, and cut threads. The main difference is the guideway layout: flat-bed machines use a horizontal arrangement, while slant-bed machines use an inclined arrangement.
This guide compares the two designs and uses the flat-bed CK6150 and slant-bed LZ-5000 as practical examples.
1. Flat-Bed vs. Slant-Bed: How Do Their Designs Differ?
A flat-bed CNC lathe has guideways arranged on a horizontal plane. This layout is common in general-purpose turning, long-shaft work, and some heavy-duty applications. Basic models often have a lower entry price, though chip buildup on horizontal surfaces needs attention.
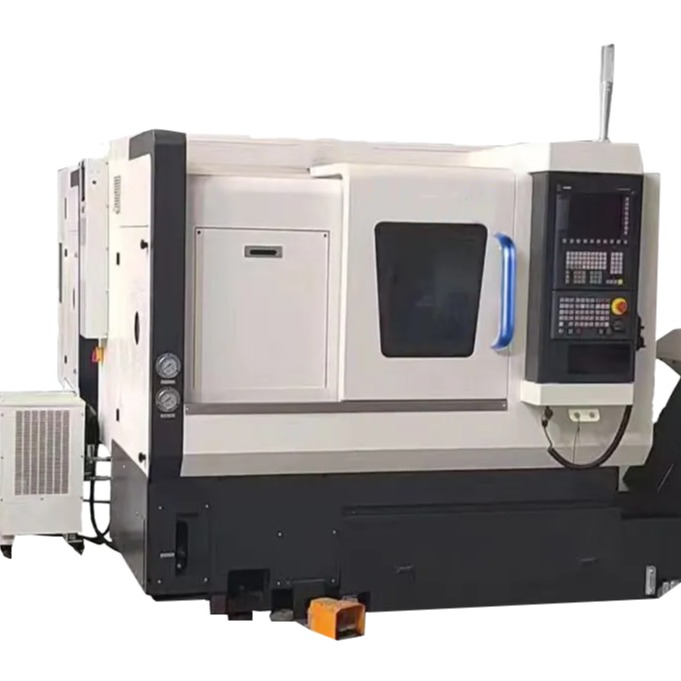
A slant-bed CNC lathe has an inclined guideway arrangement, commonly at 30° or 45°. The layout helps chips fall away from the cutting area and allows a compact arrangement of the turret and slides. It is common in machines built for repeat production.
The spindle axis normally remains horizontal on both types. Bed orientation and guideway type—such as linear guides or box ways—are separate design 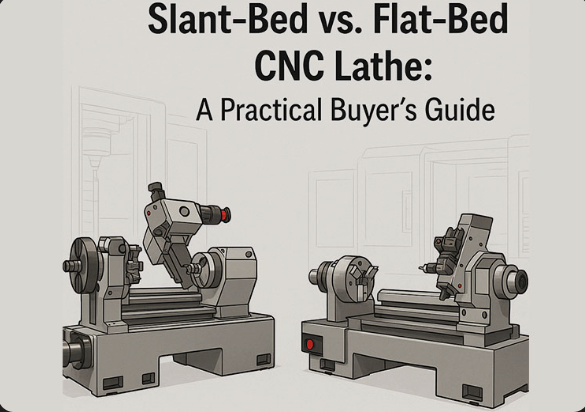
2. Key Differences at a Glance
| Feature | Flat-Bed CNC Lathe | Slant-Bed CNC Lathe |
|---|---|---|
| Guideway layout | Horizontal | Inclined |
| Chip evacuation | Horizontal areas are more prone to chip buildup; effective flushing and removal matter | Inclined layout helps chips fall away |
| Basic operations | Turning, facing, boring, and threading | The same standard turning operations |
| Material capability | Depends on the spindle, tooling, rigidity, and coolant system | Also depends on the complete machine and process |
| Common applications | General-purpose turning, long parts, and some heavy workpieces | Repeat production and compact machining cells |
| Rigidity and accuracy | Should be assessed from the machine design and cutting tests | Cannot be judged from the bed angle alone |
| Automation | Available where the layout and interfaces support it | Common in automated configurations, but equipment must be confirmed |
| Cost | Basic models often cost less initially | Fully equipped production models often require a larger investment |
How Does Chip Evacuation Affect Production Costs?
If chip buildup causes frequent stops, better evacuation can reduce cleaning interruptions and free up machining time.
For example, reducing daily chip-cleaning time from 30 minutes to 10 minutes would free up about 7.3 hours over 22 working days. This is an illustration, not a guaranteed difference between the two designs. Whether that time becomes additional output depends on demand and the rest of the production process.
A slant bed does not eliminate tangled chips. Chip breaking, coolant delivery, the conveyor, and enclosure design still matter. Less cleaning downtime may improve machine availability, but it does not translate directly into the same percentage increase in overall equipment effectiveness, or OEE.
Do Machining Functions and Suitable Parts Differ?
Both layouts support standard turning operations. Live tooling, C-axis and Y-axis functions, bar feeding, and robot loading are features that need to be checked separately.
There is no fixed material split between the two designs. Steel, stainless steel, cast iron, and aluminum should be evaluated against spindle torque, speed, tooling, and coolant capability.
| Part type | What to compare |
|---|---|
| Long shafts and sleeves | Usable machining length, tailstock, and steady-rest support |
| Discs, flanges, and rings | Actual turning diameter, workholding, load capacity, and tool clearance |
| Short shafts, bushings, and fittings | Workholding, feeding, and total cycle time |
| Heavy blanks | Permitted workpiece weight, spindle torque, and cutting-test results |
How Do Accuracy and Rigidity Affect Cost per Part?
A slant-bed lathe is not automatically more accurate than a flat-bed lathe. The casting, guideway spacing, spindle, feed system, thermal control, and workholding all contribute to the result. Compare inspection reports and actual cutting tests.
If the machine and workholding reduce vibration under the intended cutting conditions, they may reduce insert chipping, abnormal tool wear, and rework. Those savings should be verified through comparable production records rather than inferred from the bed layout.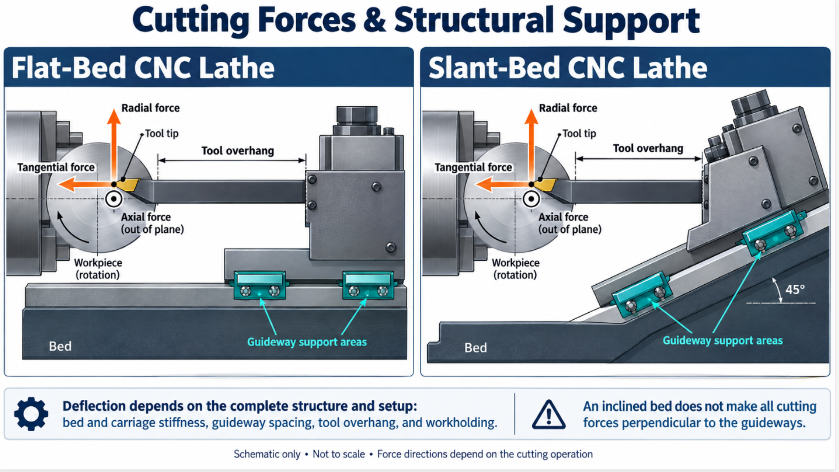
3. CK6150 vs. LZ-5000: Specifications and Reference Prices
The following example compares the flat-bed CK6150 with the slant-bed LZ-5000 using specifications available for both machines.
| Specification | Flat-Bed CK6150 | Slant-Bed LZ-5000 |
|---|---|---|
| Maximum swing over bed | 500 mm | 560 mm |
| Listed turning diameter | 260 mm, listed as maximum turning diameter at the tool post | 500 mm maximum machining diameter |
| Listed length capacity | Maximum workpiece length: 750 / 1,000 / 1,500 / 2,000 mm | Maximum machining length: 530 mm |
| CNC control | GSK; other brands optional | SYNTEC |
| Main spindle motor power | 7.5 kW | 11 kW |
| Spindle speed | Three ranges: 16–160, 120–600, and 400–2,000 rpm | Listed as 3,500 rpm; confirm whether this is the maximum speed |
| Spindle bore | 52 mm | 66 mm |
| Reference price in USD | Approximately US$14,900 | Approximately US$26,900 |
The LZ-5000 has a larger swing over bed, higher rated motor power, and a larger spindle bore. The CK6150 offers longer workpiece-length options.
However, “machining length” and “workpiece length” are different measures. The turning-diameter definitions also need confirmation before making a direct comparison.


These figures describe two specific models, not every flat-bed or slant-bed lathe.
What Does the Price Difference Mean?
The reference price difference is approximately US$12,000.
These figures were converted from RMB 100,000 and RMB 180,000 at approximately US$1 = RMB 6.70, then rounded to the nearest US$100. The exchange-rate reference date is September 23, 2026. Exchange-rate source
Whether the additional investment makes sense depends on measurable savings in labor, tooling, scrap, and downtime—or additional saleable output.
A simple starting point is:
Simple payback period = Additional installed investment ÷ Verified monthly net benefit
For example, an additional investment of US$12,000 with a verified net benefit of US$500 per month would have a simple payback period of about 24 months. This is a calculation example, not a projected return for either machine.
Prices are for reference only and do not constitute a quotation. CK6150 bed-length options, machine accessories, taxes, freight, installation, and other charges are subject to the final quotation.
4. How to Choose the Right CNC Lathe for Your Business
| Requirement | Start by considering a flat-bed model when… | Start by considering a slant-bed model when… |
|---|---|---|
| Workpiece and support | Long parts require suitable bed length and support equipment | Parts fit the working envelope and a compact layout matters |
| Production mix | General-purpose work and frequent setups are priorities | Repeated batches make chip handling and continuous operation important |
| Automation | Feeding and loading equipment can be matched to the selected machine | You plan to integrate bar feeding, parts catching, or robot loading |
| Budget | A basic configuration meets the job and initial cost is a priority | Additional production features offer a measurable benefit |
Make the final decision using the part drawing, material, tolerances, production volume, and cutting-test results. If both designs meet the requirements, compare the complete cycle time and cost per accepted part.
5. Frequently Asked Questions
Is a slant-bed lathe always more accurate?
No. Accuracy depends on the complete machine, thermal control, and workholding. Compare inspection and cutting-test results.
Can a flat-bed lathe use an automatic bar feeder?
Yes, provided the clamping system, layout, control interfaces, and supporting equipment are compatible.
Can both designs machine the same materials?
Yes, with appropriate machine specifications and cutting conditions. Bed orientation alone does not determine material capability.
Does a more expensive machine always produce a lower cost per part?
No. The extra investment needs to deliver measurable improvements in cycle time, labor, tooling, or quality—and those improvements must fit actual production demand.
How to Choose a CNC Machining Center?/cnc machining